Achieving reliable results with different models requires more than a suitable exposure time. You also need to understand which details and structures your resin can print consistently. The Phrozen RP Tester helps you evaluate thin pillars, thin walls, raised and recessed lines, holes, surface textures, and bridge structures.
This article explains how to print and interpret the Phrozen RP Tester. After completing the test, you can use the results from each area to identify the resin's strengths and limitations and choose suitable resin and support settings for different models.
Before printing the RP Tester, use the Phrozen XP Finder to determine an appropriate normal-layer exposure time. Incorrect exposure settings affect the other test areas and prevent them from accurately reflecting the resin's performance.
1 Print the Phrozen RP Tester
- Download the Phrozen RP Tester to your computer.
- Import the test model into your slicing software and apply the print settings calibrated with the Phrozen XP Finder.
- Slice the model, save it in a file format supported by your 3D printer, and transfer the file to the printer.
- Print the test piece with your 3D printer.
- After printing, wash and post-cure the test piece according to the resin manufacturer's recommendations.
- Review each test area and record the smallest feature and widest span that the resin can reproduce consistently.
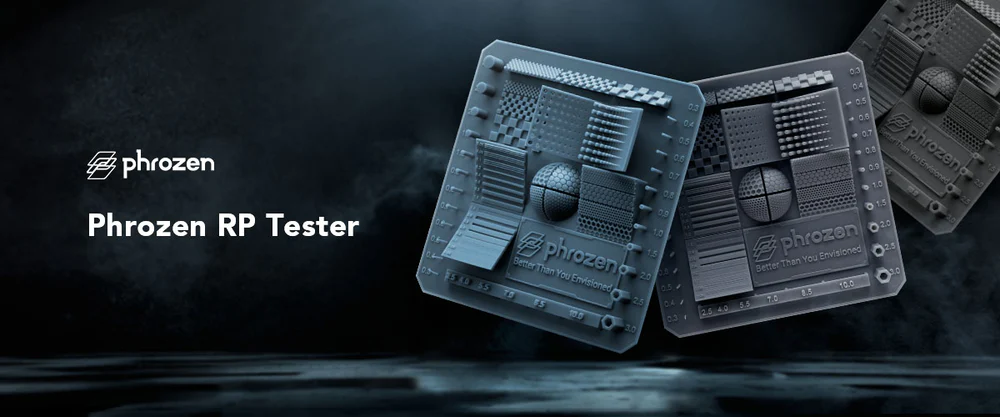
2 Review the Results
After printing the Phrozen RP Tester, first inspect the checkerboard patterns to confirm the exposure settings. Then review the pillars, sloped thin lines, pins and holes, surface textures, and bridge structures. Different resins may perform better in different areas. Use the results to decide whether a resin suits a particular model rather than to rank resins as simply good or bad.
Checkerboard Patterns
This test verifies whether the current exposure setting is appropriate. The RP Tester includes checkerboard patterns on both flat and sloped surfaces. The flat pattern primarily reflects exposure in the XY plane, while the sloped pattern more closely represents a model printed at an angle.
- With appropriate exposure, the corners of the squares should touch slightly while the boundaries remain clear.
- A visible gap between the corners usually indicates underexposure.
- Overlapping or noticeably expanded corners usually indicate overexposure.
Flat and sloped checkerboard patterns on the RP Tester (Image source: Phrozen Technology)
Pillars
The left and right sides of the RP Tester contain solid round pillars and hollow hexagonal pillars. The pillars use different diameters and wall thicknesses to show the smallest structures the resin can print consistently with appropriate exposure.
Solid Round Pillars
This test evaluates the resin's ability to form small vertical features. Ideally, the pillars should remain complete, straight, and separate from one another.
- If the thinner pillars are missing, their diameter may be below the resin's reliable printing limit.
- If a pillar forms but leans or bends, that diameter is approaching the resin's structural stability limit.
- If the pillars break easily during washing, post-curing, or handling, the resin may not suit models with many long, thin parts.
Solid round pillar results from different resins (Image source: Phrozen Technology)
Hollow Hexagonal Pillars
This test evaluates the resin's ability to form thin walls and small hollow structures. Record the thinnest hexagonal pillar that remains complete and use that result as a reference when designing thin walls or hollow details.
- If the hexagonal pillar is complete and its central opening is clear, the resin can reproduce that wall thickness consistently.
- If a thinner hexagonal pillar does not form, that wall thickness may be below the resin's reliable printing range.
- If the central opening shrinks or closes, recheck the exposure time or treat that size as the resin's detail limit.
Hollow hexagonal pillar results from different resins (Image source: Phrozen Technology)
Sloped Thin Lines
The raised and recessed lines on the sloped surface simulate textures commonly found on figures, miniatures, and other detailed models. Inspect the raised and recessed lines separately.
- The finer the raised lines that remain complete, the better the resin reproduces embossed details.
- The finer the recessed lines that remain clearly separated, the better the resin reproduces engravings and grooves.
- If raised lines break or disappear, or recessed lines become shallow or fill in, that size may be outside the resin's reliable detail range.
Raised and recessed sloped lines on the RP Tester (Image source: Phrozen Technology)
Sloped thin-line results from different resins (Image source: Phrozen Technology)
Pins and Holes
The pins and holes are placed on sloped surfaces to simulate small raised and recessed details on actual models.
Pins
- The more small pins that print successfully, the better the resin forms small raised features.
- If the thinner pins are missing, their size may be below the resin's reliable printing range.
- If the pins bend, lean, or break, the resin lacks sufficient structural stability at that size.
Sloped pin results from different resins (Image source: Phrozen Technology)
Holes
- The more complete the hole outlines and the closer their dimensions are to the model design, the better the resin reproduces small recessed details.
- If smaller holes close, the print may be overexposed or the hole size may be below the resin's detail limit.
- If the hole outlines are distorted, check the exposure settings, print stability, and whether uncured resin remains inside the holes.
Sloped holes and pins on the RP Tester (Image source: Phrozen Technology)
Flat and Spherical Textures
This test simulates complex surface textures on a model. Inspect the hexagonal patterns, the gaps between the textures, and the dividing lines on both the flat and spherical surfaces.
- Clear gaps and separated hexagons indicate that the resin can reproduce surface details at that size.
- If the hexagons merge or recessed textures fill in, check for overexposure and confirm that the test piece was washed thoroughly.
- If the flat textures are clear but the spherical textures are blurred, the resin may have more limited detail reproduction on curved or angled surfaces.
Spherical and flat textures on the RP Tester (Image source: Phrozen Technology)
Bridge Structures
The bottom of the RP Tester contains bridge structures with different spans. These structures evaluate the resin's ability to form horizontal overhangs without support.
- If a bridge remains straight, the resin can print that span consistently.
- If longer spans begin to sag, the print is approaching the resin's reliable unsupported distance.
- If the bottom of a bridge bulges, thickens, or breaks, add supports or reduce the distance between support points when printing a similar structure.
The bridge results can guide support density and spacing, but they do not replace standardized tensile-strength testing.
Bridge structure results from different resins (Image source: Phrozen Technology)
3 Additional Notes
- Every resin and printer combination is different. Use the Phrozen XP Finder to determine an appropriate normal-layer exposure time before printing the RP Tester.
- Keep one RP Tester for each resin you use regularly. Label it with the resin name, color, printer model, layer height, exposure time, and print date for future comparison.
- When comparing resins, use the same layer height, ambient temperature, washing process, and post-curing conditions whenever possible.
- Different resins may perform better in different test areas. For example, an engineering resin may not print the thinnest pillars but may remain more stable in the bridge test. Select the resin according to the model's requirements.
- RP Tester results can guide resin selection, model design, and support settings, but they do not replace the resin's technical data sheet or standardized material testing.
Contact Support
Following the steps above will help you understand how a resin performs across different structures and details. If the test piece has widespread missing features, detaches, or deforms, or if you cannot determine whether the issue is related to exposure settings, contact Phrozen Support or your authorized reseller for further assistance.
When contacting Phrozen Support, provide clear photographs of the front, side, and each test area of the RP Tester. Also include the printer model, resin name, slicing software, complete print settings, ambient temperature, washing process, and post-curing conditions.
Comments
0 comments
Article is closed for comments.